In the manufacturing industry, multi – layer pipe extrusion lines play a crucial role in producing high – quality pipes for various applications. Among the many parameters to control during the extrusion process, the layer thickness is of paramount importance as it directly affects the performance, strength, and durability of the multi – layer pipes. As a dedicated supplier of Pipe Extrusion Lines, I have witnessed firsthand the challenges manufacturers face in controlling layer thickness, and I’m excited to share some key strategies and best practices with you. Pipe Extrusion Line

Understanding the Fundamentals of Layer Thickness Control
Before diving into the control methods, it’s essential to understand the basic principles behind layer thickness in multi – layer pipe extrusion. A multi – layer pipe typically consists of several different polymer layers, each with its own specific properties and functions. For example, an outer layer may provide protection against environmental factors, while an inner layer can be designed for chemical resistance or smooth fluid flow.
The layer thickness is determined by the volume of polymer material that is extruded for each layer and the speed at which the pipe is pulled through the die. Any variation in the extrusion rate, material viscosity, or pulling speed can lead to fluctuations in layer thickness. Therefore, precise control of these variables is the key to achieving consistent layer thickness across the length and circumference of the pipe.
Extruder Control
The extruder is the heart of the multi – layer pipe extrusion process, and controlling its operation is the first step in layer thickness control. Here are some key aspects to consider:
Screw Design and Configuration
The screw in the extruder is responsible for melting, transporting, and metering the polymer material. Different screw designs are suitable for different polymer materials and extrusion requirements. A well – designed screw can ensure a uniform melt flow and accurate material metering, which are essential for consistent layer thickness. For example, a barrier screw can separate the solids and the melt phases more effectively, reducing the variation in the extrusion rate caused by inconsistent melting.
Motor and Drive System
The motor and drive system control the rotational speed of the screw. Precise control of the screw speed is necessary to maintain a constant extrusion rate. Modern extrusion lines are equipped with advanced motor control systems that can adjust the screw speed accurately in response to changes in the process conditions. For instance, if the material viscosity increases, the motor control system can increase the screw speed slightly to maintain the same extrusion rate.
Temperature Control
Temperature has a significant impact on the viscosity of the polymer material. If the temperature is too high, the material will be too thin, and if it is too low, the material will be too thick. Therefore, accurate temperature control in the extruder barrel and the die is crucial for layer thickness control. Most extrusion lines use multiple heating zones along the barrel and the die to ensure uniform temperature distribution. Temperature sensors are installed at various locations to monitor the temperature in real – time, and the heating and cooling systems are adjusted accordingly.
Die Design and Control
The die is where the different polymer layers are combined and shaped into a multi – layer pipe. The design and operation of the die have a direct influence on the layer thickness.
Die Geometry
The die geometry should be carefully designed to ensure a uniform flow of each polymer layer. The gaps and channels in the die need to be optimized to balance the pressure and flow rate of different layers. For example, in a co – extrusion die, the layer distribution plates can be adjusted to control the relative thickness of each layer. Computational Fluid Dynamics (CFD) simulations are often used during the die design process to predict the flow behavior and optimize the die geometry.
Die Temperature
Similar to the extruder, the temperature of the die also affects the layer thickness. The die needs to be maintained at a specific temperature to ensure that the polymer materials have the right viscosity for proper shaping. In some cases, different heating zones may be used in the die to control the temperature of each layer independently. This helps to compensate for any differences in the melting and flow characteristics of different polymer materials.
Die Adjustment
During the extrusion process, it may be necessary to make small adjustments to the die to correct any layer thickness variations. This can be done by using mechanical or hydraulic adjustment mechanisms. For example, shims can be added or removed from the die gap to change the thickness of a particular layer. Some advanced extrusion lines are equipped with automated die adjustment systems that can make real – time adjustments based on feedback from thickness measurement sensors.
Process Monitoring and Feedback
Continuous monitoring of the process parameters and layer thickness is essential for maintaining control. Here are some common monitoring and feedback methods:
Thickness Measurement Sensors
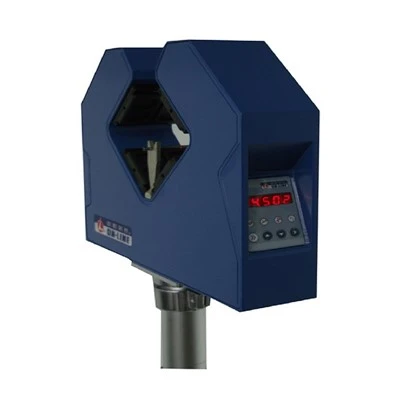
There are various types of sensors available for measuring the layer thickness of multi – layer pipes. Non – contact sensors, such as ultrasonic sensors and X – ray sensors, are often used because they can measure the thickness without touching the pipe surface, which is important for maintaining the quality of the pipe. These sensors can provide real – time thickness data, which can be used to adjust the extrusion process parameters.
Process Control Systems
Modern extrusion lines are equipped with advanced process control systems that can integrate the data from different sensors and make automatic adjustments to the extruder, die, and pulling speed. For example, if the thickness measurement sensor detects that a particular layer is too thin, the process control system can increase the extrusion rate of the corresponding extruder or adjust the die gap to correct the problem.
Operator Training and Experience
Finally, the skills and experience of the operators are also crucial for layer thickness control. Well – trained operators can recognize the signs of layer thickness variations early and take appropriate actions to correct them. They need to understand the principles of the extrusion process, the operation of the equipment, and how to interpret the data from the monitoring sensors. Regular training programs should be provided to the operators to keep them updated on the latest technologies and best practices in layer thickness control.
In conclusion, controlling the layer thickness in a multi – layer pipe extrusion line requires a comprehensive approach that involves extruder control, die design and control, process monitoring and feedback, and operator training. By implementing these strategies effectively, manufacturers can produce high – quality multi – layer pipes with consistent layer thickness, which will enhance the competitiveness of their products in the market.
Pipe Extrusion Line If you are in the market for a Pipe Extrusion Line or have any questions about layer thickness control in multi – layer pipe extrusion, I invite you to reach out to us. Our team of experts is ready to provide you with the best solutions and support for your specific needs.
References
- Menges, G., Michaeli, W., & Mohren, H. (1989). Plastics Processing: An Introduction. Hanser Publishers.
- Throne, J. L. (1996). Extrusion Dies: Design and Engineering Computations. Hanser Publishers.
- Tadmor, Z., & Gogos, C. G. (2006). Principles of Polymer Processing. Wiley – Interscience.
Zhejiang Jwell Pipe Equipment Co., Ltd.
As one of the most professional pipe extrusion line manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy cheap pipe extrusion line in stock here from our factory. Customized orders are welcome.
Address: No.128 Qingfeng Road, Xieqiao Town, Haining City, Jiaxing City, Zhejiang Province
E-mail: salaa@jwell.cn
WebSite: https://www.jwell-pipe.com/
